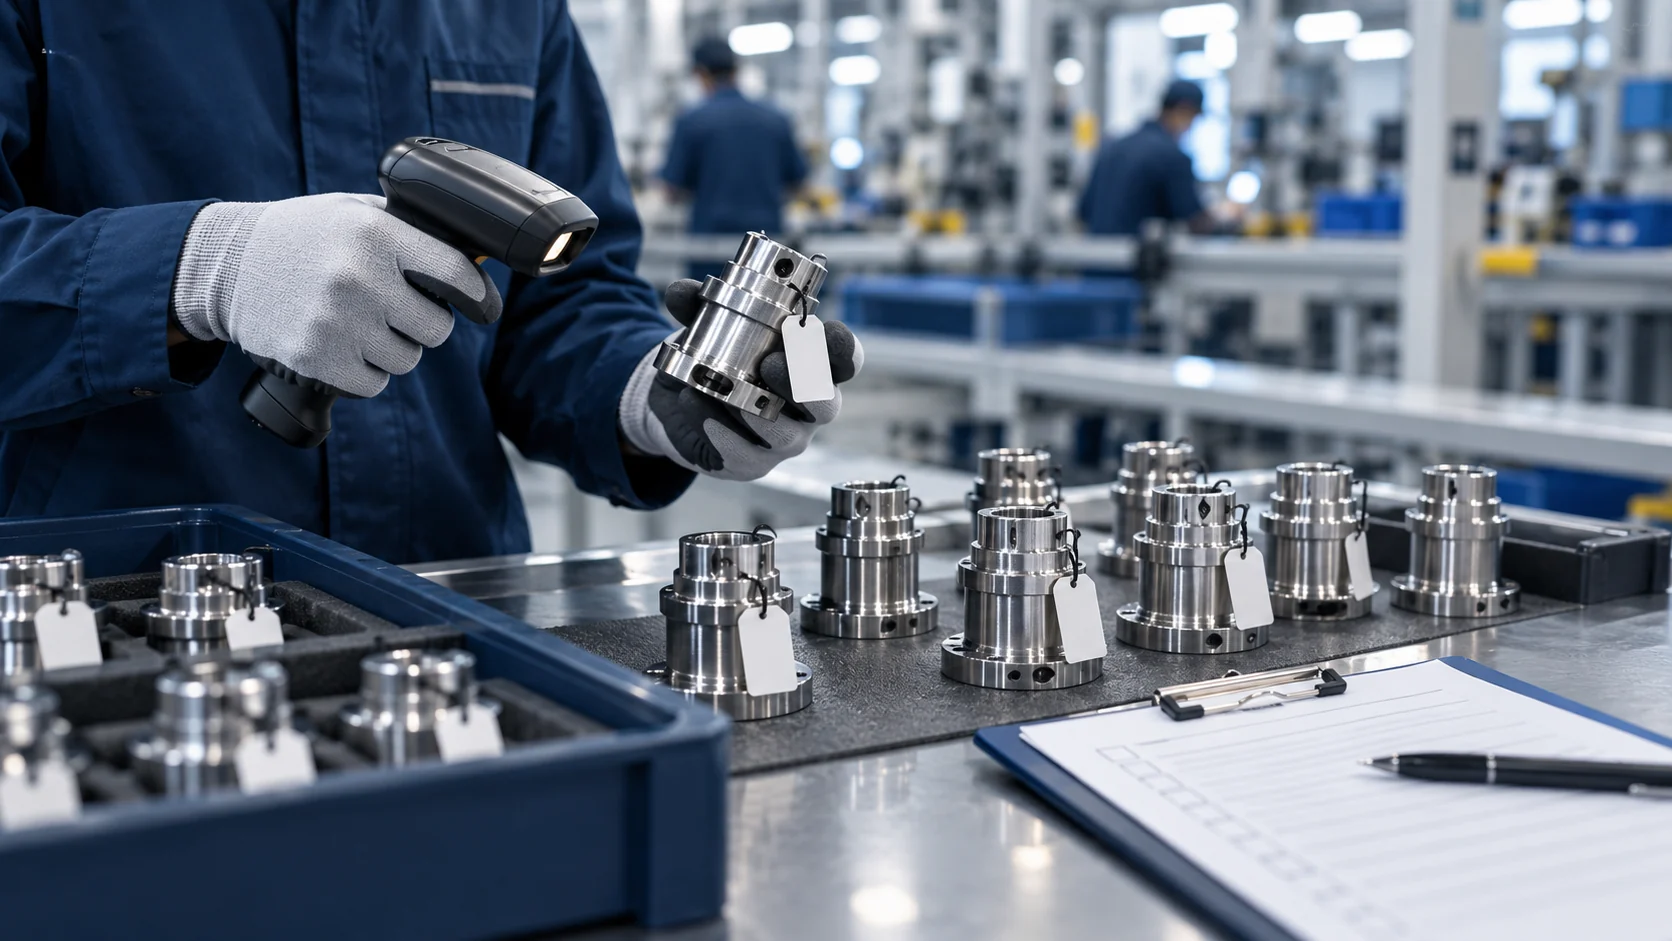
Manufacturing quality, operations, and compliance
Item-level traceability is the ability to identify each individual unit of production, follow its materials, work orders, inspections, and destinations, and connect that history to a verifiable mark on the unit itself. Most traceability programs are built on software that records scans of printed labels and assumes the identifier is trustworthy. This guide covers the layer those systems assume: choosing lot versus item granularity, selecting marking that survives your process, and closing the gap between a physical unit and the record that describes it.
Buyers: plant, quality, compliance teams
Layer: physical identity plus records
Goal: audit-ready unit genealogy
Key takeaways for manufacturing and quality leaders
- Item-level traceability means unit genealogy, not just batch bookkeeping. Each unit carries a unique identity that links work orders, materials, inspections, and destinations in one chain.
- Software records scans; it does not prove the mark is genuine. Copied labels, swapped tags, and destroyed codes quietly disconnect records from reality.
- Granularity is a risk decision. Lots are cheap but inflate recall scope; serial or item marking pays for itself where safety, regulation, warranty, or brand exposure is high.
- Mina links overt and covert codes on the same unit. If the visible code is destroyed, the ultra-invisible code, readable only with dedicated detection devices, keeps the unit tied to its record.
- Acceptance testing decides the project. Mark durability through your real process, readout reliability, and device governance must be proven before serialization scales.
What is item-level traceability?
Item-level traceability is the ability to identify each discrete unit of production and reconstruct its history: which material lots and components went into it, which work order and process steps touched it, which inspections released or rejected it, and which destination it shipped to. Traceability runs in two directions: backward from a suspect unit to its inputs, and forward from a suspect input to every affected unit.
The concept is distinct from lot tracking. A lot is a group of units that share a batch, heat, reel, or production run, so one identifier covers many units. Item-level identification gives each unit its own identity. Industry practice, reflected in manufacturing software guides, treats lots as efficient for commodities and bulk materials, and serial or item identity as the fit for high-value, safety-critical, repairable, or regulated parts.
Standards already push in this direction. Since its 2015 edition, ISO 9001 has required organizations to control the unique identification of outputs and retain the documented information that enables traceability whenever traceability is a requirement, a requirement carried forward as the standard is updated. Automotive quality management under IATF 16949 goes further with a documented, risk-based traceability plan and enhanced traceability for safety, regulatory, or otherwise critical parts. Medical device manufacturers under ISO 13485 must document procedures that define the extent of traceability and keep distribution records for each batch.
Where traceability programs break: the identifier layer
The main failure mode of a traceability program is silent divergence between records and reality. A scan creates a database entry; nothing in the database proves that the scanned label was the one applied to that unit at that station. When a label is copied, a tag is moved, a code is abraded off in a wash or curing step, or an operator keys a serial by hand, the record chain continues to look complete while pointing at the wrong physical unit.
The consequences are expensive precisely where traceability is supposed to protect the business. A GMA and Deloitte survey of 36 food, beverage, and consumer product companies found that the direct costs of a recall average about US$ 10 million per event, before lost sales and brand damage. Broad lot-level identity forces wider containment than necessary, so every ambiguity in the record expands the recall, the quarantine, and the investigation.
Compliance exposure follows the same pattern. An auditor asks you to demonstrate that a specific serialized unit in the field was produced on a specific date from a specific material lot. If the visible mark on that unit can be forged, duplicated, or was destroyed in service, the demonstration depends on paperwork alone, and paper genealogy without a physical anchor is exactly what sophisticated counterfeiters and diverters exploit.
Lot versus item granularity: a decision, not a default
Choosing granularity is the first procurement decision, because marking method, data volume, and recall scope all follow from it. The decision table below reflects how the trade-off behaves in practice.
| Situation | Fit | Why |
|---|---|---|
| Commodity inputs, bulk materials, packaging film | Lot-level | Units are interchangeable; per-unit numbering adds cost without changing containment decisions |
| Regulated or safety-critical components | Item-level | IATF 16949-style enhanced traceability and targeted recalls need unit identity |
| Warranty, service, and returns management | Item-level | Serial identity matches a returned unit to its production and service history |
| High-value parts exposed to counterfeiting or diversion | Item-level with covert layer | Visible-only codes can be copied; a hidden code defends the record-to-unit binding |
| Mixed lines with shared platforms | Hybrid | Item identity at final assembly, lot identity for sub-components, all linked in the genealogy |
A practical rule: serialize where a unit can fail alone, be serviced alone, or be counterfeited alone. If a quality escape can only ever be handled as a batch, lot identity is sufficient; the moment a single unit must be found in the field, item identity earns its cost.
Marking technology comparison for item identity
Once granularity is chosen, the physical carrier decides whether the identity survives your process and your product’s life. The comparison below covers the common routes and their behavior in the field.
| Option | Typical use | Main weakness |
|---|---|---|
| Printed label with barcode or 2D code | High-volume consumer goods, cartons, labels scanned at stations | Labels peel, abrade, and can be reprinted or duplicated by outsiders |
| Laser or dot-peen direct part marking | Metal and plastic components in durable-goods assembly | Visible marks can be ground off; engraving alone does not resist relabeling attacks |
| RFID tag | Reusable assets, pallets, high-value logistics | Cost per unit, read-range interference, and tag removal or transfer |
| Inkjet or printed serial on the product | Primary packaging in regulated lines | Solvents, sterilization, and abrasion can erase it; visible codes invite copying |
| Mina overt code plus ultra-invisible covert code | Units and packaging needing audit-proof record linkage | Covert reads require dedicated devices and trained, authorized staff |
The defining property of the last row is not invisibility alone; it is the interrelation of the two codes. Manufacturing software, including MES-based traceability systems, assumes the scanned identifier is authentic and focuses on capturing machine, material, and labor data against it. No mainstream software stack answers how a physical label is prevented from being forged, lost mid-production, or transferred between units. That gap sits exactly at the point where Mina’s technology operates. If you are comparing marking suppliers more broadly, Mina’s procurement framework for evaluating invisible security ink suppliers covers the questions to ask.
How Mina keeps marks and records linked
Mina’s one-item-one-code approach assigns each unit a unique identity carried by two linked layers: an overt code for everyday scanning and an ultra-invisible code that cannot be seen under normal light, ultraviolet light, or infrared light and cannot be read by conventional equipment. The two layers are related by design, so when a visible code is scratched off, painted over, or damaged in service, the covert code still identifies the unit and keeps it tied to its recorded history.
Verification uses dedicated detection devices that Mina supplies only to its partner clients, each device carrying a unique identification number. Audio verification returns sound and vibration on a genuine marked unit and no reaction otherwise; image verification displays the covert information where it was placed. This makes field checks fast: an auditor or inspector can confirm a unit’s identity in seconds, at goods-in, on the line, or in the field, without a laboratory.
The same identity feeds the record chain. Mina’s traceability concept covers the process from production to distribution, monitoring production nodes and quality checkpoints under one code per item, and its audit workflow lets authorized staff log in, scan the code, and read the distribution information recorded against that item. For consumer-facing products, a phone-readable AI cloud code adds a public verification layer without special equipment, and query records such as first scan time and scan counts expose duplicated codes.
Positioning matters here. Mina is the identification and verification layer: the durable physical identity on the unit, the controlled reading of that identity, and the linkage of that identity to distribution and inspection information. The plant’s own systems remain the system of record for process data, and Mina’s layer is what makes their key, the identifier, defensible. Marking can be integrated into existing labels, packaging, and printing without changing designs, and in-material marking is available for ceramics, plastics, rubber, and related carriers; a published Mina application, serialized ceramic hand formers marked with codes that survive kiln firing, shows this working as an internal asset-tracking system on a live production line.
Acceptance testing and rollout workflow
Treat the marking project like any process qualification. The following workflow qualifies the identifier layer before serialization scales.
- Map units, records, and failure modes. Decide which items carry identity, which events create records, and how you will answer an auditor’s question for one unit, end to end.
- Choose marking points per process. Identify where marks are applied and every hazard they must survive: washes, curing, sterilization, surface treatment, assembly, and field use.
- Build test panels. Assemble genuine marked units, unmarked units, copied visible codes, and marks damaged by your actual process steps. Inspectors must distinguish every panel member correctly.
- Run durability and readout acceptance tests. Verify overt codes scan through the full line, covert codes read with each detection device, and both survive environmental exposure and simulated aging, with rechecks after cleaning and rework cycles.
- Stand up device and data governance. Register every detection device and holder, define who may verify and how results are logged, and set retention that satisfies your quality and regulatory record rules.
- Escalate and audit. Define the path from a failed field check to quarantine, investigation, and supplier action, then audit verification logs periodically for duplicate identities and anomalies.
Keep the pilot on one line and one product family first. Scale serial issuance only after the acceptance report shows the binding between unit and record holds through your worst process step.
Standards alignment and governance
Governance turns marking into evidence. Under ISO 9001, when traceability is a requirement you must control the unique identification of outputs and retain the documented information that enables it, so record retention and identifier issuance rules belong in the quality system, not in a vendor’s defaults. Automotive programs should map marking coverage to the IATF 16949 risk-based traceability plan and demonstrate enhanced traceability for safety and regulatory parts, where individual marking is the expected route. Medical device programs align with ISO 13485, which requires documented traceability procedures, defined extent, and distribution records per batch.
Identifier issuance deserves explicit controls. If a supplier, licensee, or distributor can print your identifiers, the record chain inherits their discipline. Governing identifier supply through the brand, the model Mina applies to its brand licensing and label control programs, keeps issuance tied to actual authorized production quantities.
Finally, decide data ownership before rollout: who holds serial allocations, verification logs, and first-scan records, how long they are retained, and in what format auditors can query them. Traceability data that cannot be exported and explained years later does not meet the retention intent of any of these standards.
Limitations and risks to state openly
Item-level traceability has real limits, and a program is stronger when they are explicit. Identity is not genealogy: a durable code proves which unit is in front of you, but the completeness of its history still depends on capture discipline at every station. If operators skip scans or records are incomplete, the identifier cannot reconstruct events nobody logged.
The covert layer has operational dependencies. Reads require dedicated devices in the right hands, so coverage, training, and device custody must be planned; a missing covert signal after physical damage is inconclusive and should be escalated, not treated as proof of counterfeiting. And serialization itself has cost: per-unit marking, data volume, and query infrastructure only pay off where unit-level risk exists, which is why the granularity decision comes first.
Mina’s layer does not replace your MES or ERP. Process data capture, integrations, and record systems remain the plant’s responsibility and architecture; Mina supplies the physical identity, the controlled verification, and the distribution linkage. Overclaiming integration scope is how traceability projects fail audits.
FAQ: item-level traceability
What is item-level traceability?
It is the ability to identify each individual production unit and reconstruct its full history, materials, work orders, inspections, and destination, by a unique identity carried on the unit itself, running both backward to inputs and forward to affected units.
What is the difference between lot and item traceability?
Lot traceability assigns one identifier to a batch of units that share a production run; item traceability gives each unit its own identifier. Lots are cheaper but force broader containment, while item identity enables targeted recalls and unit-level warranty and audit evidence.
Which standards require traceability?
Since the 2015 edition, ISO 9001 has required controlling unique identification of outputs and retaining traceability records when traceability is a requirement. IATF 16949 adds a documented, risk-based traceability plan and enhanced traceability for safety and regulatory parts. ISO 13485 requires documented traceability procedures and distribution records for medical devices.
Why is a printed barcode not enough for audit-proof traceability?
A barcode records whatever was scanned, and a copied, moved, or destroyed label breaks the link between the record and the physical unit. A covert code that survives visible-code damage keeps the unit tied to its record even after the public identifier is gone.
How do field teams verify a Mina-marked unit?
With dedicated detection devices supplied to partner clients: audio verification returns sound and vibration on a genuine unit and no reaction otherwise, and image verification displays the covert information. Each device has a unique identification number and is not sold on the open market.
What should be tested before scaling serialization?
Test panels of genuine, unmarked, copied, and process-damaged units; mark durability through your worst process steps and simulated aging; readout reliability with every detection device; and the device, issuance, and retention governance that makes results auditable.
Sources
- ISO 9001 quality management systems standard page (2015 edition, superseded by ISO 9001:2026)
- IATF 16949 automotive quality management standard, IATF Global Oversight
- ISO 13485:2016 medical devices quality management standard page
- GMA and Deloitte: Capturing Recall Costs whitepaper
- JobPack: manufacturing traceability software, lot and serial tracking
- Symestic: traceability in manufacturing, serial, batch, and MES data
Next step for an item-level traceability program
If your records need an identifier that survives the process and stands up to audits, prepare a brief with your product families, process hazards the mark must survive, granularity targets, and the regulatory standards you answer to. Mina can evaluate overt-plus-covert marking for your units and packaging and propose an acceptance test plan. Item-level traceability starts with one unit, one identity, and one honest test.
Contact Mina Anti-counterfeiting Technology for a technical consultation
Explore Mina’s traceability cloud platform to scope identifiers, event capture, record lookup and enterprise or consumer access for your production workflow.